Manufacturing
Manufacturing infrastructure
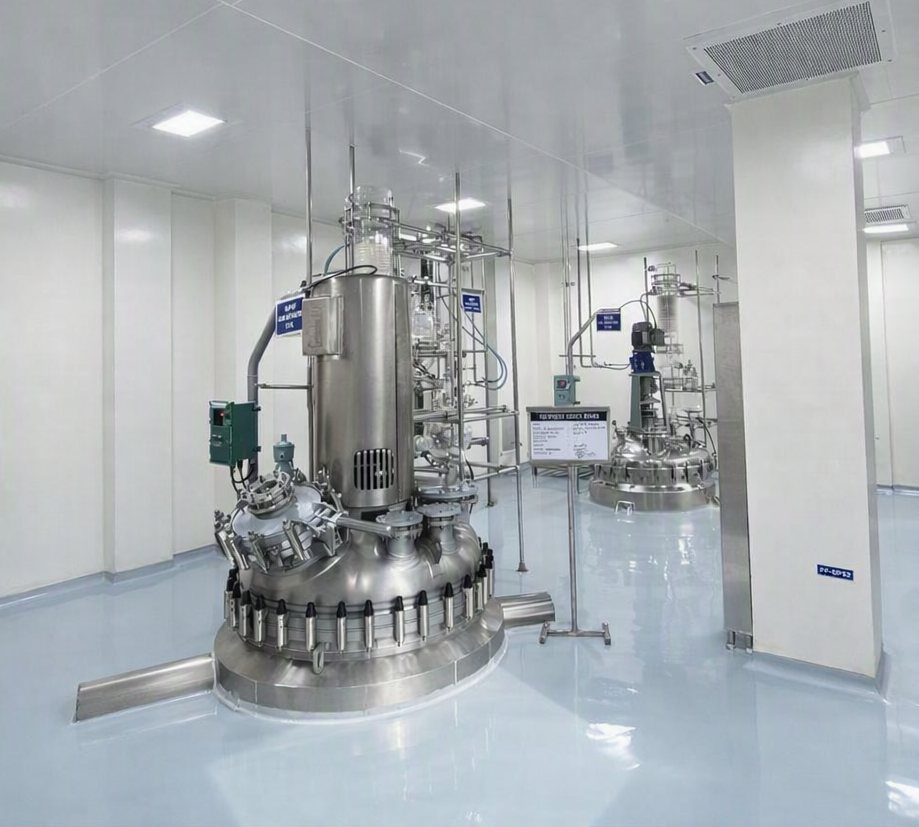
Our modern manufacturing facility supports pilot-scale development through commercial-scale production of pharmaceutical intermediates, APIs, and specialty chemicals. The plant is designed for operational flexibility, process reliability, safe chemical handling, and consistent product quality.
Inside the plant
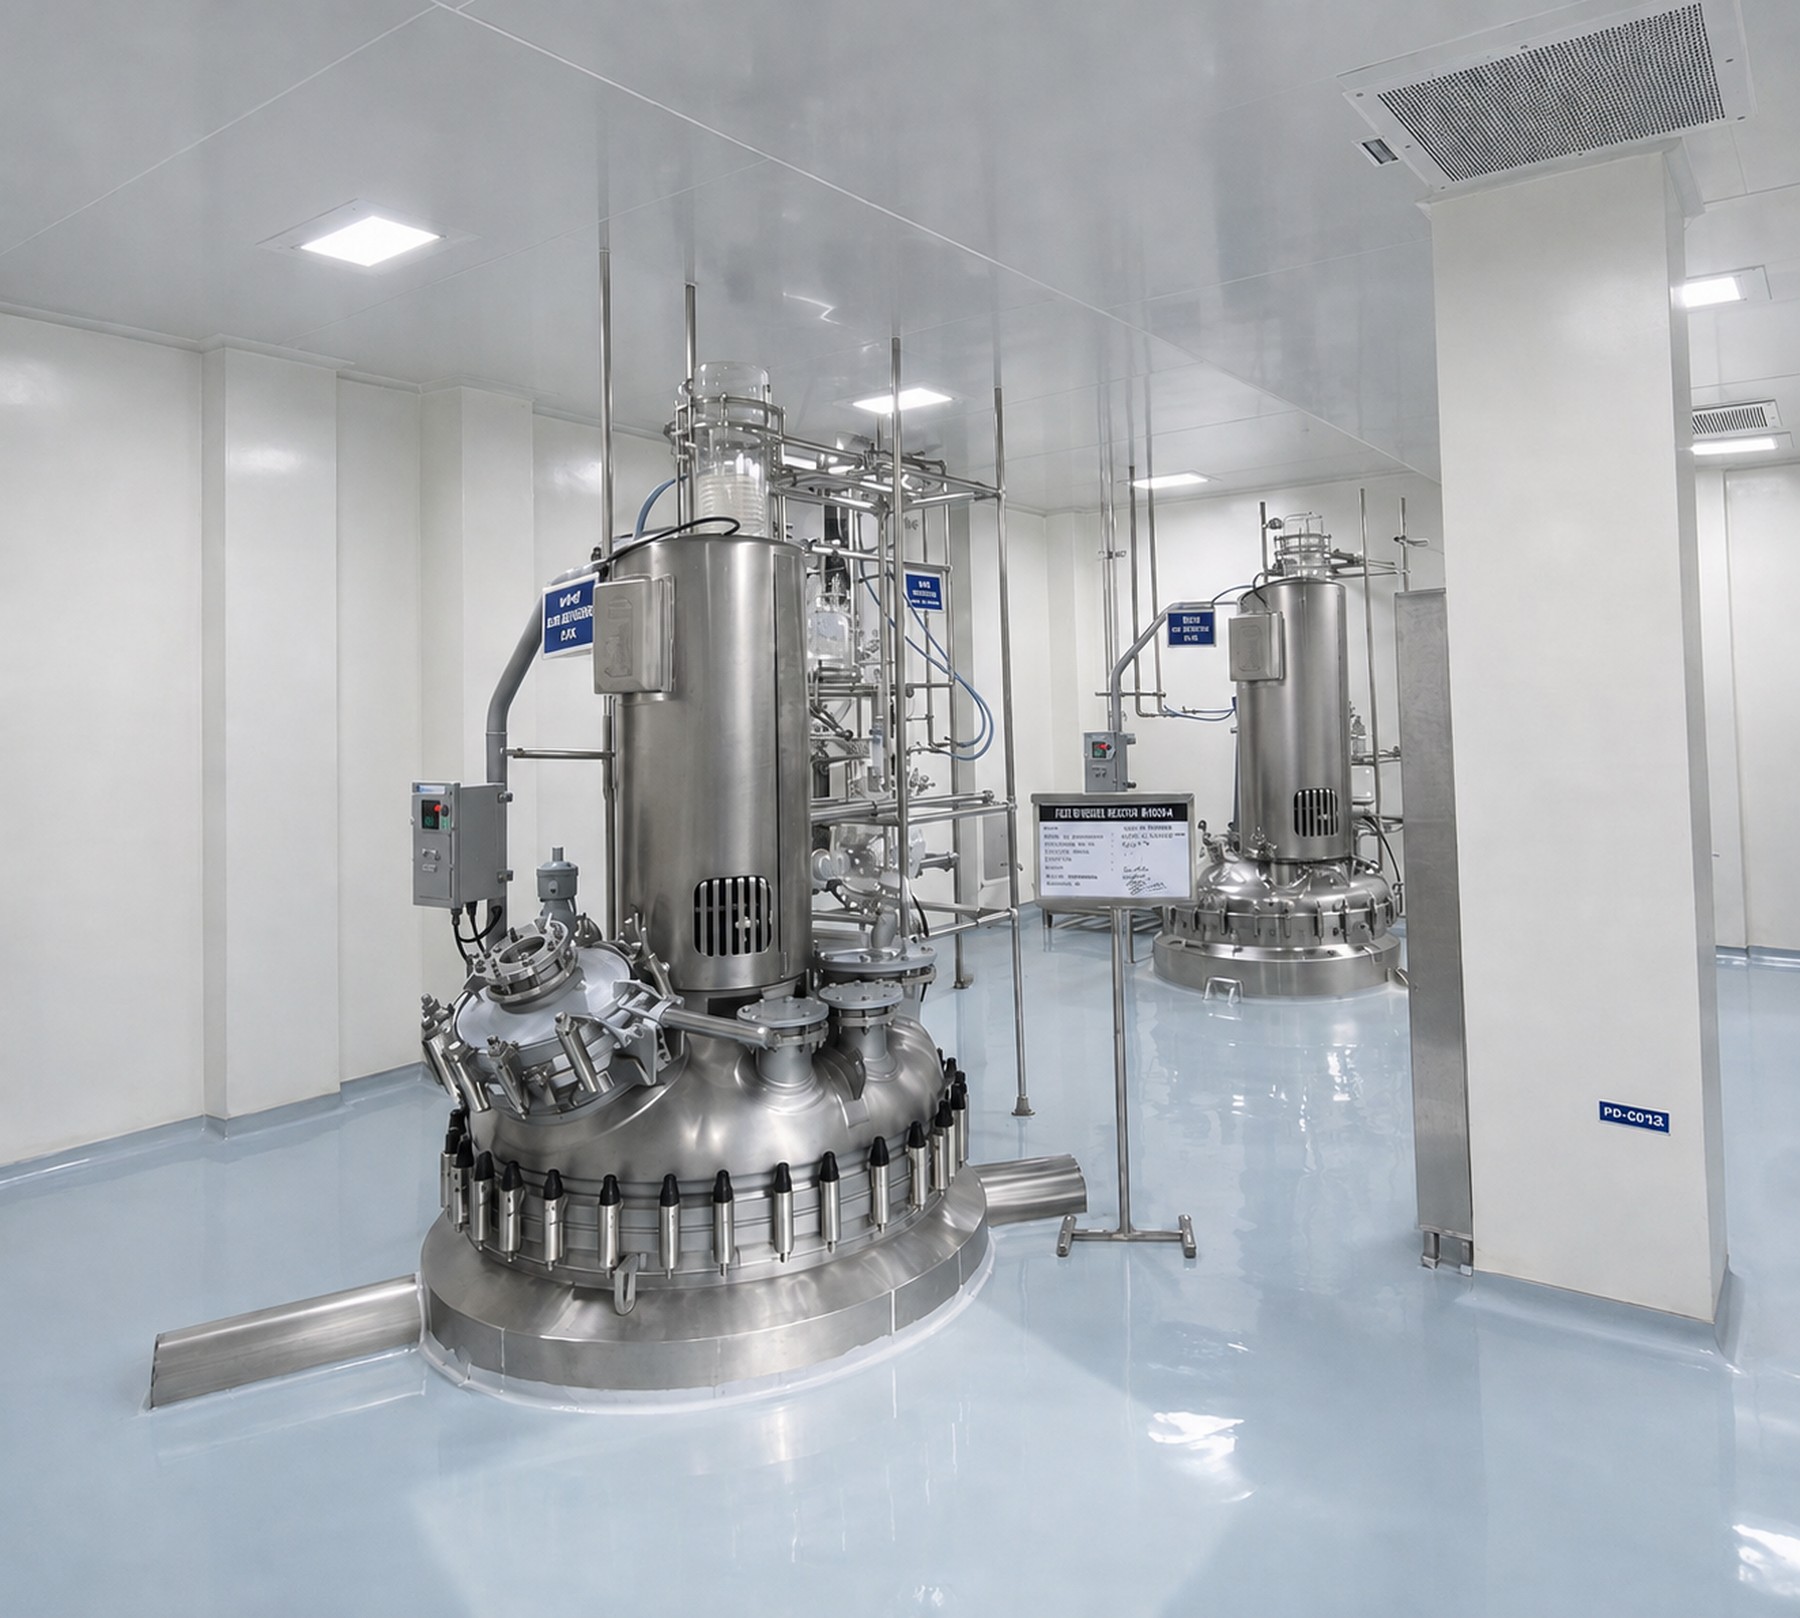
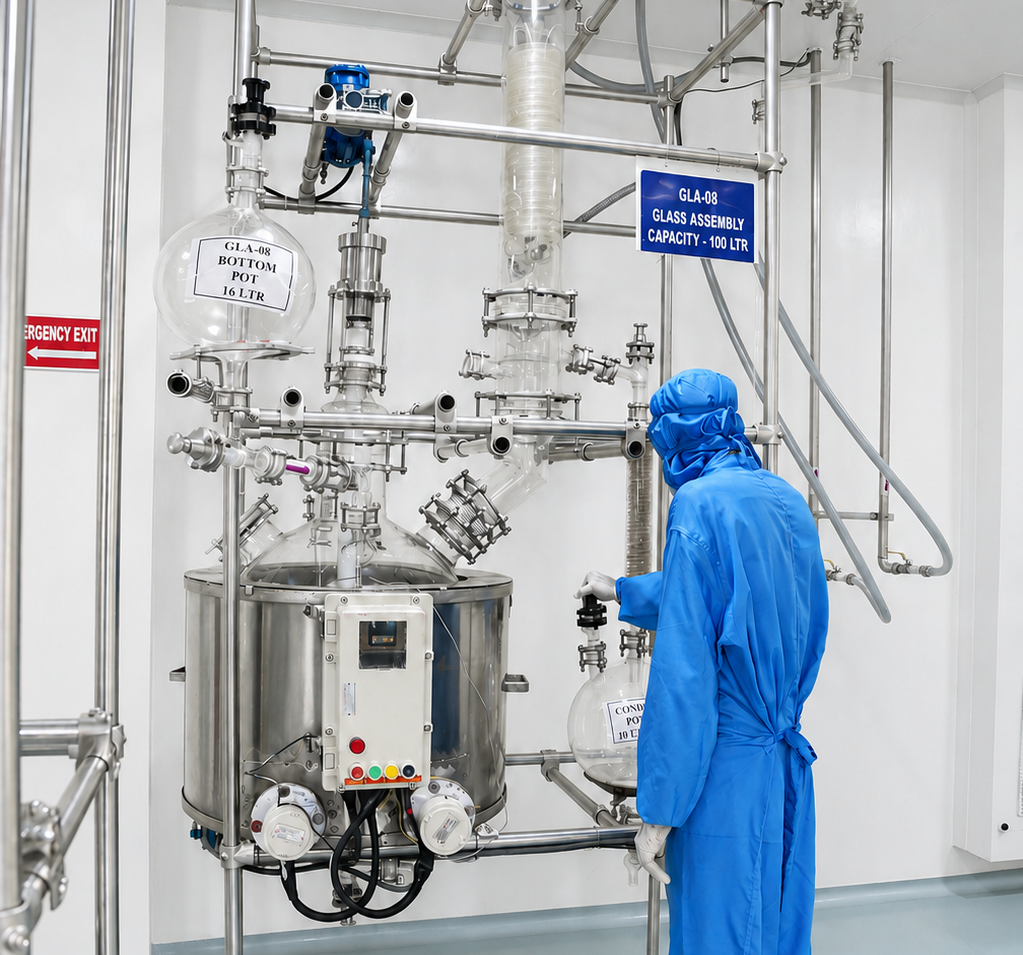
Reactor hall, classified area
Reactors, condensers and process piping laid out for clean material flow, safe handling and straightforward cleaning between campaigns.
Dedicated production blocks
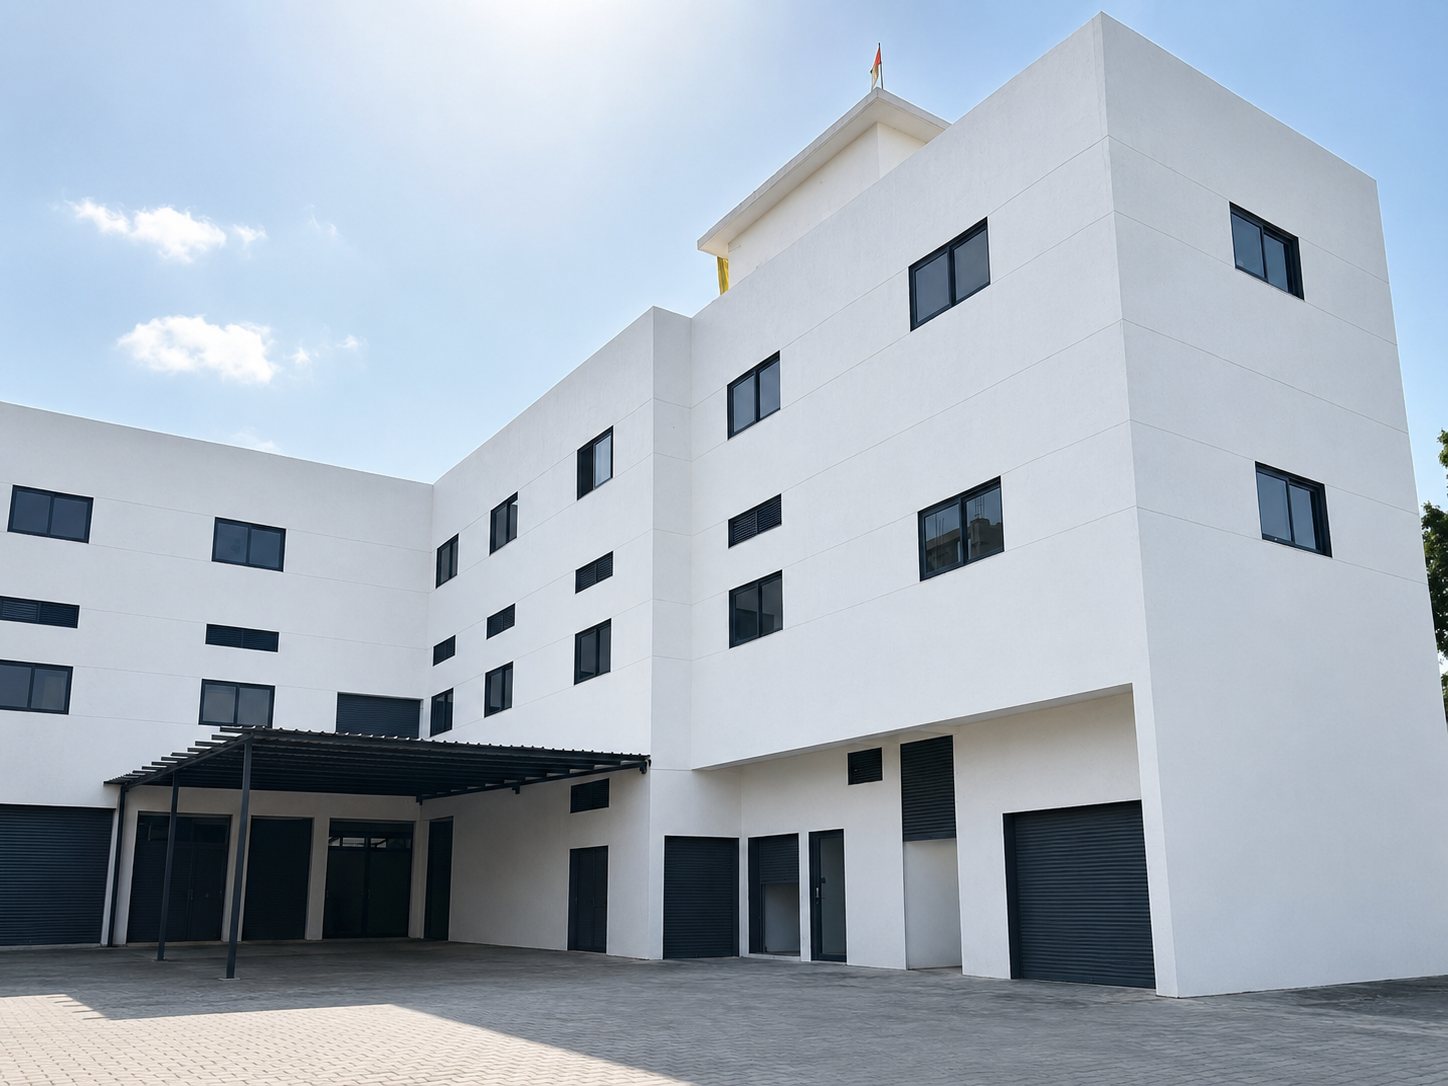
Two blocks, cleanly separated
Segregated production areas support contamination control, efficient production planning, and the operational discipline required for diverse product portfolios.
Block 1
Intermediate area
Pharmaceutical intermediates, specialty chemicals, and advanced chemical intermediates.
Block 2
Classified area
Active pharmaceutical ingredients (APIs).
Core reaction capabilities
Chemistry we run every day
These capabilities enable the manufacture of a broad range of high-value intermediates and APIs for pharmaceutical and specialty chemical applications.
- Iodination
- Esterification
- Bromination
- Diazotization
- Cyclization
- Grignard reactions
- Condensation reactions
Reactor systems
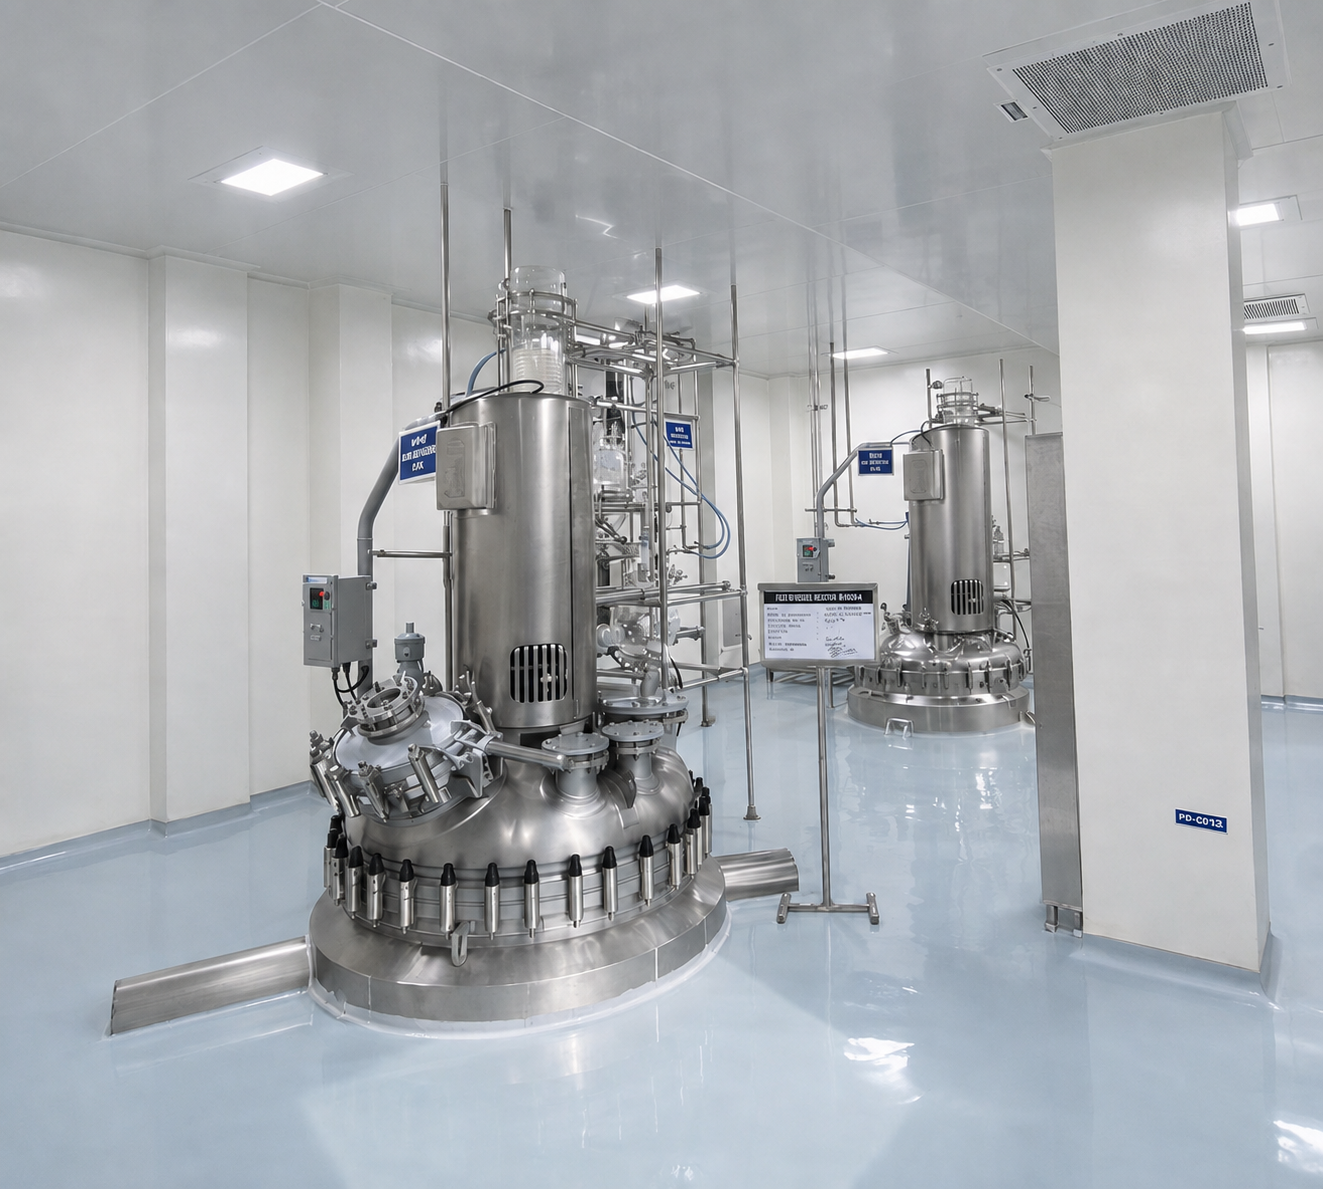
Reactor Types and Capacities
| Glass-lined reactors | 200 L to 8000 L |
|---|---|
| Stainless-steel reactors | 1000 L to 5000 L |
| Borosilicate glass reactors | 50 L to 500 L |
Process equipment
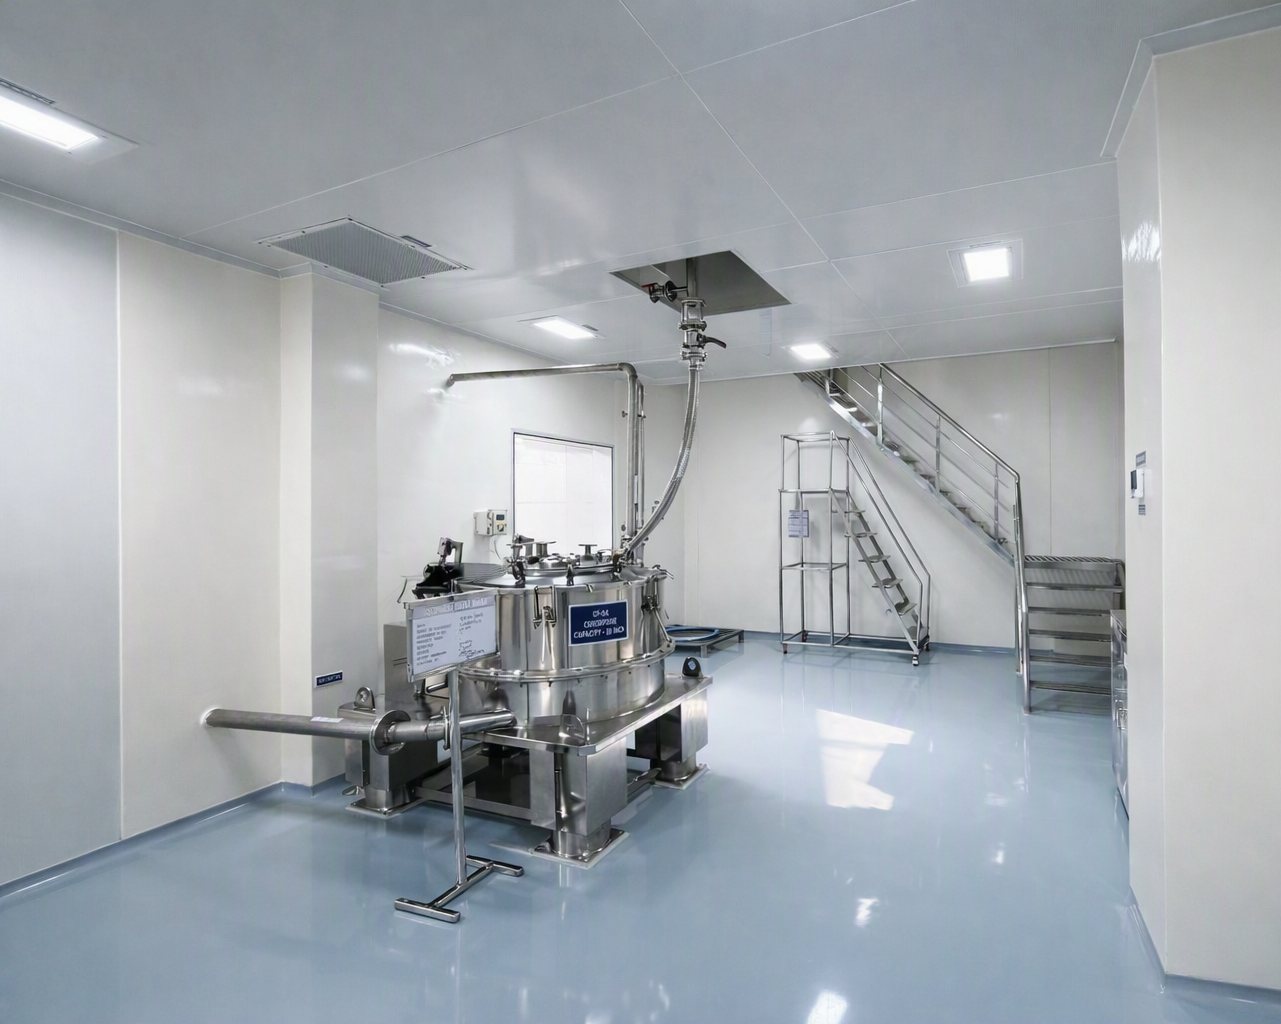
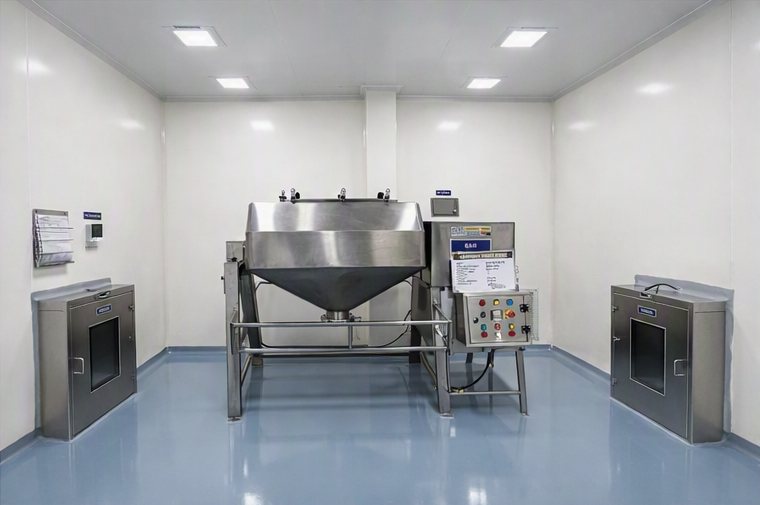
Downstream and finishing
- Centrifuges — 5 units
- Dryers — 3 units
- Nutsche filter
- Blender
- Multi mill
- Evaporator
- Sifter
- Other allied process equipment
Storage & warehousing
Controlled storage, end to end
Dedicated warehouse areas support the controlled storage of raw materials and finished products for both intermediate and API operations.
- Segregated storage for raw materials and finished products
- Inventory identification and traceability
- Controlled storage conditions, where applicable
- Safe material movement and handling practices